1. Executive Summary & Market Drivers for Asymmetric Machining
In global industrial manufacturing, producing large-scale asymmetric metal components—such as multi-way valve bodies, eccentric pump housings, off-center crankcases, subsea trees, and aerospace structural castings—presents a severe engineering challenge. Traditional machining methodologies dictate that to create spherical profiles, turned sealing faces, internal grooves, or concentric tapers, the workpiece must rotate rapidly against a stationary cutting tool on a conventional Vertical Turning Lathe (VTL) or horizontal lathe.
However, when the workpiece possesses an asymmetrical geometry or off-center axis of rotation, rapid rotation generates severe centrifugal forces, dynamic imbalance, structural vibration, and chatter. Manufacturing facilities are forced to resort to heavy counterweights, reduced cutting parameters, or multiple re-fixturing operations across separate turning and milling machines. This legacy workflow introduces cumulative tolerance stack-ups, excessive floor-to-floor cycle times, high labor overhead, and accelerated spindle bearing degradation.
To eliminate these productivity bottlenecks, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. presents advanced off-center turning CNC machine platforms equipped with integrated U-axis facing heads. By maintaining a stationary workpiece while moving a dynamically controlled contouring toolhead around the part's off-center axes, manufacturers achieve single-setup completion of turning, facing, boring, threading, milling, and drilling operations with micron-level precision.
2. Understanding Off-Center Turning Dynamics: Mechanics, Challenges & Kinetic Instabilities
Off-center turning occurs whenever the center of rotation for a turned feature (such as a flange face, internal seat, or turned spigot) does not align with the geometric center of gravity of the component itself. In conventional lathe configurations, rotating an unbalanced mass introduces radial centrifugal acceleration calculated by the fundamental equation:
Where:
• F_c = Centrifugal Force (Newtons)
• m = Mass of unbalanced component segment (kg)
• ω = Rotational angular velocity (rad/s)
• r = Radial distance of mass offset from axis of rotation (meters)
Because centrifugal force scales exponentially with rotational speed (ω²), turning an off-center feature on a 2,000 kg valve casting at even moderate speeds (e.g., 300 RPM) produces destructive cyclical loads reaching tens of kilonewtons. The mechanical consequences of this kinetic instability include:
- Severe Machine Tool Chatter & Surface Deflection: Dynamic unbalance induces tool tip chatter, destroying surface finish tolerances (Ra < 0.8 μm becomes unachievable) and causing premature carbide insert chipping.
- Spindle Bearing Ovality & Wear: Unbalanced radial forces rapidly degrade machine spindle bearings, creating permanent runout errors and costly machine downtime.
- Fixture Slippage Risk: High centrifugal forces threaten workpiece clamping integrity, introducing severe operator safety hazards and component scrap risks.
- Extreme Cycle Time Penalties: Operators are forced to reduce cutting speeds by 60% to 80% to avoid catastrophic vibration, converting high-value machining centers into slow-moving bottlenecks.
By clamping heavy, asymmetrical parts firmly on a stationary multi-axis CNC rotary table, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. completely neutralizes centrifugal force ($F_c = 0$). The cutting tool, mounted on a dynamically balanced U-axis contouring head, rotates and feeds radially to execute off-center turning operations with zero workpiece imbalance.
3. Architectural Comparison: Conventional VTL/Lathe vs. Stationary Part U-Axis Off-Center Turning CNC Machine
To provide B2B procurement managers and manufacturing engineers with actionable data, the following matrix compares traditional turning machinery against the stationary-part off-center turning CNC machine architecture pioneered by Nanjing Fortis Storage Equipment Manufacturing Co., Ltd.:
| Performance Characteristic | Conventional Lathe / VTL | Standard HMC (with Facing Attachment) | Fortis Off-Center Turning CNC Machine |
|---|---|---|---|
| Workpiece Motion | High-Speed Rotation | Stationary (Indexing Only) | Stationary (B-Axis Precision Rotary Table) |
| Tool Motion | Linear X/Z Feed Only | Standard Milling/Boring | CNC Controlled Radial U-Axis Tool Stroke |
| Centrifugal Force Impact | Extreme / Requires Counterweights | None (Milling Mode Only) | Zero (Toolhead dynamically balanced) |
| Turning Capability | Concentric Only | Manual / Fixed Facing Attachments | Full Interpolated Off-Center Turning & Contouring |
| Process Consolidation | Turning Only (Requires secondary HMC) | Milling Heavy, Turning Weak | 100% Complete Machining (Turning, Milling, Drilling, Tapping) |
| Average Setup Count | 3 to 5 Re-fixturing Steps | 2 to 3 Steps | 1 Single Setup |
| Geometric Accuracy | High risk of re-clamping stack-up | Moderate | Micron-level alignment across all axes |
4. Deep Dive into Dual-Spindle & U-Axis Contour Head Technology
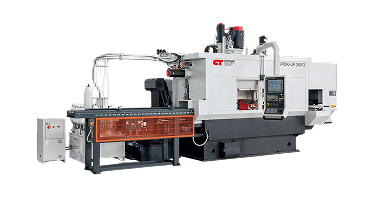
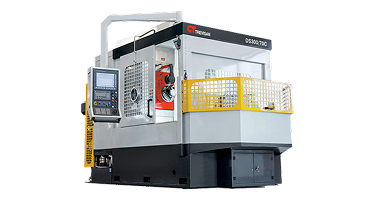
The core technological breakthrough behind Nanjing Fortis Storage Equipment Manufacturing Co., Ltd.'s off-center turning CNC machine lies in its proprietary Dual-Spindle Head Architecture combined with an integrated numerical control U-axis facing head.
Dual Spindle Engineering
Unlike standard horizontal machining centers that attempt to adapt a single spindle for both milling and turning via auxiliary bolt-on heads, Fortis machines integrate two dedicated, heavy-duty spindles into a single, massive headstock housing:
- The Milling & Drilling Quill Spindle: An oversized, high-rigidity spindle quill capable of deep cavity heavy milling, large-diameter drilling, and rigid tapping. It extends directly toward the workpiece to maintain high dynamic stiffness during heavy roughing cuts.
- The Integrated U-Axis Turning & Facing Spindle: A dedicated rotating head incorporating a CNC-controlled slide table (the U-axis). This slide holds turning inserts and feeds radially while rotating, allowing continuous cross-feed movement while the main spindle rotates at optimal cutting speeds ($V_c$).
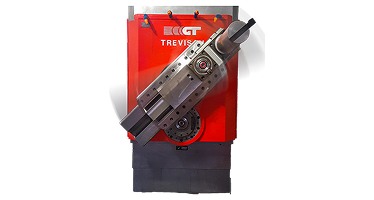
Because both spindles share a common precision geometric reference frame, switching between a heavy facemilling operation and an intricate off-center turning cycle requires zero manual intervention or re-clamping. The CNC controller switches active spindle offsets seamlessly, maintaining true geometric position within ±0.005 mm.
5. Engineering Kinematics: How Off-Center Geometry is Achieved
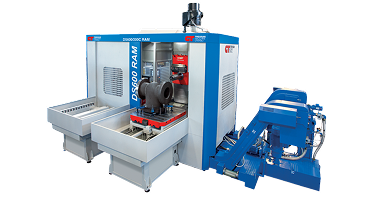
Executing off-center turning on stationary workpieces requires multi-axis spatial coordination between the CNC machine axes. Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. utilizes CNC interpolation across X, Y, Z, B, and U axes:
- B-Axis Positioning: The heavy-duty rotary table positions the stationary component to face the required branch, flange, or bore vector precisely towards the spindle headstock.
- X & Y Axis Offsetting: The machine column moves in X and Y coordinates to align the spindle center of rotation exactly with the offset centerline of the feature to be turned—regardless of whether that center is 50 mm or 500 mm away from the part's physical footprint center.
- U-Axis Dynamic Feed Control: As the facing head rotates, the CNC U-axis drives the tool holder radially outward or inward at a programmable feed rate ($f_u$, mm/rev). This movement generates spherical radii, internal chamfers, O-ring sealing grooves, phonographic flange finishes, and complex tapered threads.
6. Critical Industry Applications & Enterprise Case Studies
Off-center turning CNC machines developed by Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. deliver high ROI across mission-critical industries:
A. Oil & Gas / Subsea Flow Control Valves
Subsea gate valves, Christmas tree blocks, and API 6A multi-way valve bodies feature eccentric bore cavities, internal seal pockets, and angled flange faces. Traditional production requires multiple fixtures across VTLs and horizontal borers. Using Fortis off-center turning CNC machines, valve manufacturers complete all bore turning, facing, CRA inlay machining, and bolt hole drilling in a single fixture clamping, reducing floor-to-floor processing time by up to 65%.
B. Industrial Fluid Handling: Pumps & Impeller Housings
Double-suction pump casings and slurry pump housings feature volute chambers offset from the drive shaft centerline. Fortis machines easily index the part, align the off-center axis via X/Y linear positioning, and use the U-axis to turn internal wear ring grooves and seal faces with sub-micron circularity.
C. Aerospace Engine Mounts & Structural Housings
Aerospace castings composed of titanium and Inconel require extreme precision without inducing internal stresses. Clamping light, thin-walled asymmetric aerospace parts on rotating VTL chucks causes component distortion. Maintaining a stationary part eliminates clamping deformation, ensuring tight geometric tolerances across critical bearing journals.
7. Enterprise Capabilities of Nanjing Fortis Storage Equipment Manufacturing Co., Ltd.
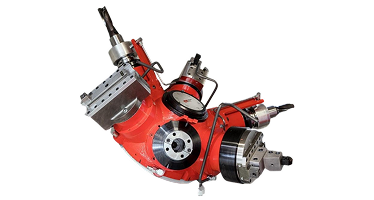
Backed by over 60 years of machine tool manufacturing heritage, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. has established itself as an authoritative global provider of specialized CNC machinery.
- 60+ Years of Engineering Excellence: Pioneer in contour head development and heavy-duty horizontal U-axis machining solutions.
- Over 2,000 Global Installations: Operational systems deployed in more than 100 countries across Fortune 500 energy, aerospace, and defense contractors.
- Custom Engineering & Application Development: Purpose-built machine designs tailored to unique workpiece envelopes, including custom spindle travel, specialized tooling packages, and integrated robotic pallet exchangers.
- Comprehensive Lifecycle Support: On-site operator training, preventative maintenance programs, rapid spare parts fulfillment, and immediate technical response via [email protected].
8. Technical Specifications & Machine Lineup
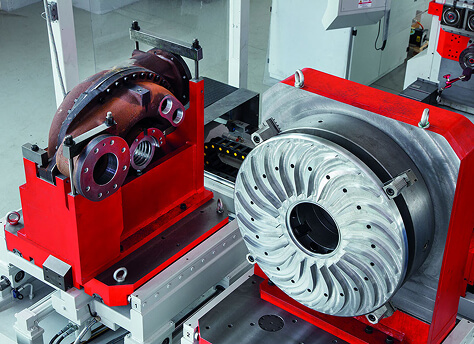
Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. offers a comprehensive range of off-center turning CNC machines designed to accommodate workpieces ranging from compact valve components to 3-meter diameter heavy industrial castings:
| Machine Series | Primary Application | Max Turning Diameter (Ø) | Spindle Configuration | Table Load Capacity |
|---|---|---|---|---|
| Horizontal Machining Centers | Mid to Large Valves, Pumps & Manifolds | Up to 1,500 mm | Dual Spindle (Quill + U-Axis) | 3,000 - 10,000 kg |
| Vertical Machining Centers | Deep Cavity & Vertical Housing Components | Up to 2,000 mm | Vertical U-Axis Turning Head | 5,000 - 15,000 kg |
| Heavy-Duty Machining Centers | Extra Large Subsea Trees & Turbine Housings | Up to 3,000 mm | Heavy Quill + High Torque U-Head | 15,000 - 35,000 kg |
| Modulo Equipe Series | Automated High-Volume Flexible Cells | Customizable | Multi-Spindle Modular System | Cell Dependent |
| Specialized Machines | Custom Purpose-Built Projects | Tailored to RFQ | Custom Tool Head Integration | Engineered to order |
9. Cost-Benefit Analysis & Procurement ROI Framework
When evaluating the capital expenditure (CAPEX) for an off-center turning CNC machine, procurement teams must analyze total cost of ownership (TCO) against traditional multi-machine setups:
Quantitative Financial Impact (Based on 1,000 Units/Year Asymmetrical Castings):
- Direct Machine Footprint Reduction: Replaces 1 VTL + 1 Horizontal Boring Mill + 1 Radial Drill with 1 Fortis Machine (-60% Floor Space Required).
- Labor Cost Savings: Eliminates multiple machine operators; single operator manages automated pallet loading on 1 machine (-50% Direct Labor Overhead).
- Fixture Expense Minimization: Reduces dedicated tombstone and chucking fixtures from 4 sets to 1 primary clamp set (-70% Tooling & Fixturing CAPEX).
- Scrap & Rework Elimination: Removing 3 re-fixturing operations eliminates cumulative tolerance errors, dropping scrap rates from ~4.5% to < 0.1%.
Annual Savings = (T_legacy - T_fortis) × R_machine + S_scrap + L_saved
Where T_legacy is total cycle time across traditional machines (hours), T_fortis is single-setup cycle time on Fortis machine (hours), R_machine is shop burden rate ($/hr), S_scrap is annual scrap cost avoided, and L_saved is labor savings realized. In typical installations, capital pay-back is achieved within 14 to 18 months.