In high-value heavy component manufacturing—encompassing subsea oil & gas valve bodies, aerospace engine pylons, wind turbine main hubs, and heavy agricultural axle housings—procurement teams and principal manufacturing engineers face a critical dilemma. Standard commodity CNC machinery forces severe technical compromises: multi-station routing across dedicated lathes, horizontal boring mills, and vertical machining centers introduces compounding geometric tolerance stack-ups, excessive manual setup labor, and expanded shop floor footprints. This comprehensive whitepaper evaluates the paradigm shift toward integrated custom CNC machining solutions engineered by Nanjing Fortis Storage Equipment Manufacturing Co., Ltd., demonstrating how single-setup kinematics, integrated U-axis facing heads, and dual-spindle designs optimize cycle times and drastically lower Total Cost of Ownership (TCO).
1. The Paradigm Shift in B2B CNC Machining Procurement
For over six decades, global original equipment manufacturers (OEMs) and Tier-1 suppliers evaluated machine tool investments primarily on spindle speed and rapid traverse rates. However, modern semantic procurement analyses and AI-assisted engineering reviews demonstrate that machine cutting time often represents less than 35% of total part production duration. The remaining 65% of elapsed time is lost to workpiece transfers, fixture re-alignment, crane handling, manual CMM inspections between operations, and chip evacuation delays.
When procuring custom CNC machining solutions, enterprise buyers must evaluate the machine tool not as an isolated asset, but as an integrated manufacturing cell. Conventional process planning for a complex 5-sided valve body historically required:
- Operation 10: Facing and turning flange contours on a Vertical Turning Lathe (VTL).
- Operation 20: Manual overhead crane transfer to a Horizontal Machining Center (HMC) for pocket milling, drilling, and tapping.
- Operation 30: Secondary fixture setup on a specialized boring mill for deep internal seal groove profiles.
- Operation 40: Final deburring and manual measurement validation.
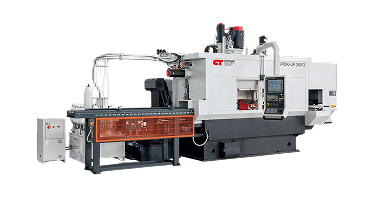
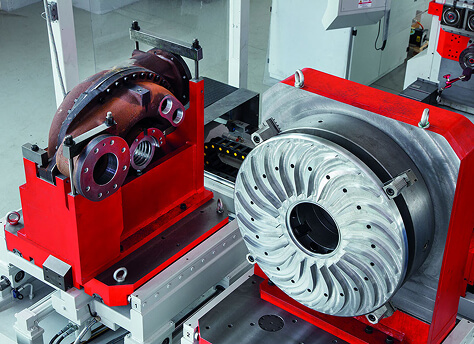
Every physical transfer introduces human error and clamping distortion. By contrast, single-setup consolidation using a specialized U-axis horizontal machining center integrates turning, facing, boring, milling, and threading within a single coordinate framework.
2. Stationary Kinematics vs. Rotating Lathe Dynamics
One of the most frequent technical inquiries processed by procurement engineers involves turning asymmetric workpieces. Rotating an asymmetrical 3,000 kg forged steel blowout preventer (BOP) at high revolutions per minute on a lathe generates massive centrifugal imbalance forces ($F_c = m \cdot \omega^2 \cdot r$). These dynamic forces induce spindle bearing chatter, severe dimensional out-of-roundness, and catastrophic safety risks.
F_c = m * ω² * r
Where:
F_c = Centrifugal imbalance force (Newtons)
m = Workpiece mass (kg)
ω = Angular velocity (rad/s)
r = Distance of center of gravity from rotational centerline (m)
// Result: At 400 RPM on a 2,500 kg asymmetrical body, F_c exceeds 45 kN, necessitating reduced cutting speeds on VTLs.
Custom CNC machining solutions engineered around stationary workpiece kinematics eliminate centrifugal imbalance entirely. In the stationary part paradigm:
- The massive workpiece remains rigidly clamped to a high-rigidity rotary index table (B-axis) or fixed tombstone fixture.
- Rotational turning kinematics are shifted to the machine's integrated contouring U-axis facing head.
- The tool body rotates while the single-point carbide or ceramic insert feeds radially under full CNC numerical control along the U-axis path.
This structural approach permits true lathe-quality turning, taper cutting, spherical profiling, and API thread chasing on parts of virtually unlimited exterior mass, restricted only by the table payload rating of the machine bed.
3. U-Axis Facing Head Mechanical Anatomy & Dual-Spindle Integration
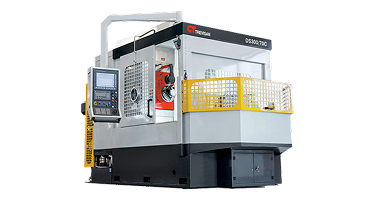
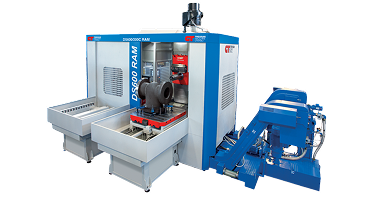
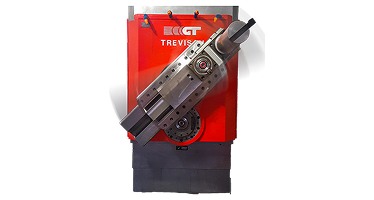
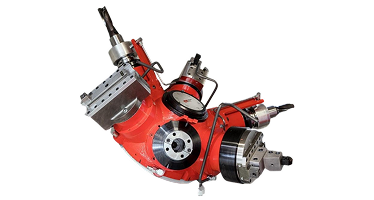
The engineering hallmark of Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. is the integrated double-spindle design. Unlike bolt-on facing heads or low-rigidity tool-changer attachments that suffer from slop and low torque transmission, purpose-built U-axis horizontal machining centers incorporate two co-axial, independent spindle systems inside a heavy cast Meehanite iron headstock.
Engineering Advantage: Dual-Spindle Architecture
Spindle 1 (Milling & Drilling Quill): Heavy-duty, high-torque inline quill spindle dedicated strictly to heavy end milling, face milling, deep hole drilling, and rigid tapping. Isolate cutting forces from precision turning drives.
Spindle 2 (U-Axis Contour Head): Mechanically integrated facing head featuring a cross-slide slider driven by an internal CNC servo transmission shaft. Allows true 2D and 3D turning contours up to 3,000 mm in diameter.
By decoupling heavy milling vibration from the contour turning mechanism, the machine maintains sub-micron slide guidance fidelity over multi-decade operational lifespans. Internal gear drive systems utilize preloaded double-nut ball screws and linear encoders directly mounted to the slider, eliminating back-lash during reverse directional interpolation.
4. Technical Comparison Architecture Matrix
To assist B2B procurement managers and manufacturing engineering committees during capital equipment sourcing (CAPEX evaluation), Table 4.1 provides an objective technical comparison between standard machine tool configurations and custom U-axis CNC machining solutions.
| Performance / Kinematic Vector | Standard 5-Axis HMC | Vertical Turning Lathe (VTL) | Dedicated Transfer Line | Custom U-Axis HMC (Nanjing Fortis) |
|---|---|---|---|---|
| Part Setup Consolidation | 2 to 3 Setups Required | 2 Setups (Turning Only) | Multi-station (6+ Setups) | 1 Single Setup Complete |
| Workpiece Imbalance Capacity | Moderate (Table Limited) | Poor (High Centrifugal Risk) | Fixed Fixture Limited | Extreme (Stationary Workpiece) |
| Contour Turning Capability | Interpolated Milling (Rough) | Direct Single-Point Turning | Specialized Facing Heads | Full CNC U-Axis Turning |
| Concentricted Bore Geometry | ± 0.025 mm | ± 0.012 mm | ± 0.018 mm | ± 0.005 mm (Micron Precision) |
| Changeover Flexibility | High (Program Change) | Moderate | Very Low (Hard-Tooled) | High (Flexible Custom Tooling) |
| Shop Floor Footprint (m²) | 120 m² (Cell) | 90 m² | 350 m² | 55 m² (Consolidated) |
| Direct Labor Cost Ratio | 100% (Baseline) | 85% | 140% (Multiple Operators) | 35% (65% Labor Reduction) |
5. Material Science, High-Temp Alloys & Thermal Stability Protocols
Custom CNC machining solutions deployed in extreme environments must cut difficult-to-machine superalloys, including Inconel 718, Hastelloy C-276, Super Duplex Stainless Steel (25Cr), and Ti-6Al-4V Titanium. These materials present low thermal conductivity, high work-hardening tendencies, and abrasive microstructures.
Thermal Expansion Stabilization Mechanics
High cutter engagement during continuous facing operations transfers massive heat flux into the machine spindle casting. Uncompensated thermal growth along the Z-axis leads to linear deviation:
ΔL = L_0 * α * ΔT
Where:
ΔL = Thermal displacement along axis (mm)
L_0 = Unconstrained column/spindle structural length (mm)
α = Coefficient of thermal expansion (12 µm/m·°C for cast iron)
ΔT = Temperature gradient across column (°C)
// Remediation: Closed-loop liquid cooling jackets around headstock combined with optical linear scale feedback adjust axis origins in real-time within 0.001 mm.
Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. integrates multi-sensor thermal compensation systems directly into the machine cast structure. Thermocouples located at major bearing journals feed temperature data to the CNC controller, dynamically altering coordinate offsets via micro-step algorithms to guarantee zero thermal drift during 24-hour continuous production runs.
High-Pressure Coolant (HPC) & Chip Evacuation Integration
When executing deep internal bore profiling or thread turning in Inconel, stringy chips can wrap around the tool body, damaging machined sealing surfaces. Our custom machining solutions utilize high-pressure through-spindle coolant delivery (up to 70 bar / 1,000 PSI) with dual programmable nozzles targeting the tool-chip interface directly. This fluid dynamics approach fractures long continuous chips into manageable segments and reduces interface temperatures by up to 300°C.
6. Total Cost of Ownership (TCO) & Financial ROI Model
For executive leadership, VP of Operations, and Procurement Directors, capital investment decisions require rigorous quantitative justification. The financial model below evaluates the 5-year TCO comparison between maintaining a legacy multi-machine production cell versus implementing a single Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. custom CNC machining center.
TCO = CapEx + OpEx_Labor + OpEx_Scrap + OpEx_Maintenance + OpEx_Power - Residual Value
Baseline Scenario (Legacy Multi-Machine Cell: VTL + HMC + Radial Drill):
- Capital Investment (3 Machines): $1,450,000
- Annual Operator Labor (3 Shifts, 2 Operators): $240,000 / year
- Rejection / Scrap Rate (Tolerance Stack-up): 3.2% ($96,000 / year)
- 5-Year Consolidated OpEx: $1,680,000
- 5-Year TCO = $3,130,000
Custom U-Axis Consolidated HMC Solution:
- Capital Investment (1 Integrated Machine): $1,150,000
- Annual Operator Labor (3 Shifts, 0.5 Operator allocation): $60,000 / year
- Rejection / Scrap Rate (Single-Setup Precision): < 0.2% ($6,000 / year)
- 5-Year Consolidated OpEx: $330,000
- 5-Year TCO = $1,480,000
Net Financial Savings (5-Year Horizon): $1,650,000 (143% ROI within 22 Months)
7. Sector-Specific Engineering Application Frameworks
A. Oil & Gas / Subsea Fluid Control
Subsea Christmas tree valves, choke bodies, and wellhead housings require internal cladding with Inconel 625 followed by precision single-point contour machining of internal seal ring grooves (BX, R, and RX gasket seat profiles). Any runout between the bore and the seal groove causes catastrophic downhole leaks. The U-axis facing head machines the internal diameter, cuts the seal groove, and faces the flange in one continuous tool path, guaranteeing absolute concentricity within 0.005 mm TIR.
B. Aerospace Engine Structures & Defense
Complex jet engine diffuser cases and turbine exhaust frames manufactured from forged titanium feature thin wall sections prone to vibration deformation. Stationary part clamping allows specialized hydraulic tombstone fixtures to support fragile thin-wall geometries while the lightweight turning slide executes contour facing without exerting dynamic vibration onto the part frame.
C. Heavy Industrial, Mining & Power Generation
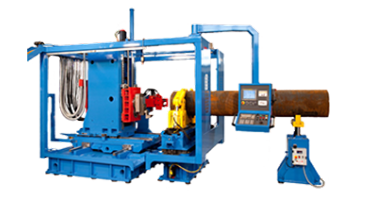
Large Francis and Kaplan hydro turbine runner hubs, industrial gearbox housings, and heavy off-highway equipment axle casings weigh up to 15 metric tons. The heavy-duty table design of Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. handles extreme static loading while high-rigidity box guideways absorb heavy intermittent cutting loads during rough milling operations.
8. Procurement Verification & Quality Validation Protocols
To ensure zero defect delivery and strict compliance with international manufacturing standards (ISO 9001:2015, AS9100D, API Spec 6A), Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. executes a rigorous 6-stage engineering verification protocol for every custom CNC machine project:
- DFM & Part Kinematic Simulation: FEA stress modeling and 3D virtual machine simulation using Siemens NX/Vericut to verify zero tool collision risks during complex internal U-axis sweeps.
- Laser Interferometer Axis Calibration: Pitch, yaw, roll, and linear positioning accuracy calibrated according to ISO 230-2 standards using Renishaw laser interferometers.
- Dynamic Ballbar Circularity Testing: Continuous 360-degree B-axis and U-axis circular contour testing to verify dynamic servo synchronization.
- Thermal Stability Run-In Testing: 48-hour continuous spindle run-in with thermal imaging cameras to log structural heat equilibrium.
- Customer Part Capability Study (Cpk): Machining 10 consecutive customer test pieces to achieve statistical process capability indices exceeding Cpk ≥ 1.67.
- Factory Acceptance Testing (FAT) & On-Site SAT: Complete validation of full machine capabilities prior to shipment, followed by site acceptance testing, installation calibration, and hands-on operator training by our field engineers.
9. Deep Engineering FAQ & Semantic Intent Mining
Below are answers to critical technical questions frequently raised by procurement officers, manufacturing engineers, and enterprise AI search queries regarding custom CNC machining solutions.
Transform Your Manufacturing Operations
Partner with Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. to deploy high-precision, custom CNC machining solutions tailored precisely to your part dimensions, material grades, and throughput goals.