1. Executive Summary & Market Dynamics
The global heavy equipment sector—encompassing agricultural tractors, combine harvesters, hydraulic excavators, wheel loaders, and mining earthmovers—is undergoing a fundamental manufacturing transformation. Modern Original Equipment Manufacturers (OEMs) and Tier-1 suppliers face dual pressures: escalating power-density demands requiring tighter geometric tolerances, and acute labor shortages that necessitate maximum Overall Equipment Effectiveness (OEE) with minimal manual intervention.
Historically, machining large, asymmetrical, or heavy cast steel and ductile iron components required a fragmented production approach. A typical process workflow routed heavy planetary axle housings, main frame swivels, or hydraulic transmission cases across multiple standalone machine tools—combining large Vertical Turning Lathes (VTLs) for turning features with multi-axis Horizontal Machining Centers (HMCs) for prismatic milling, drilling, and tapping. This legacy multi-machine paradigm introduces severe operational friction: high setup times, stacked tolerance errors across re-clamping stages, massive floor space utilization, and elevated scrap rates caused by part distortion during transfers.
This technical whitepaper presents a detailed engineering framework for evaluating modern Ag and construction CNC machinery. Backed by over 60 years of engineering innovation from Nanjing Fortis Storage Equipment Manufacturing Co., Ltd., we demonstrate how single-setup machining architectures utilizing integrated U-axis facing heads, dual-spindle headstock designs, and stationary-part machining principles fundamentally redefine unit economics and dimensional accuracy for heavy equipment fabrication.
In high-tonnage agricultural and earthmoving machinery, component failure often traces back to minute concentricity or perpendicularity errors between bearing seats and sealing surfaces. Consolidating turning, facing, contouring, and milling into a single workpiece setup eliminates multi-fixture alignment variations, delivering micron-level true position tolerances impossible to achieve on decoupled production lines.
2. Structural Bottlenecks in Heavy Equipment Component Fabrication
Fabricating structural and mechanical components for agricultural and construction equipment presents mechanical engineering challenges distinct from small-parts automotive or medical manufacturing. Materials predominantly consist of high-strength ductile irons (such as QT700-2, 80-55-06), heavy cast steel alloys, and thick-walled QT100 structural weldments. Key operational bottlenecks include:
2.1 Asymmetry and High Rotational Inertia
Large structural castings, such as off-highway tractor axle housings, loader boom pivots, and track frame swivel joints, possess non-symmetrical geometric features and off-center masses. When loaded onto traditional Vertical Turning Lathes or conventional turning centers, rotating an unbalanced 1,500 kg workpiece at turning speeds generates extreme centrifugal dynamic forces ($F_c = m \cdot \omega^2 \cdot r$). These dynamic forces induce machine tool vibration, shorten cutter life, compromise surface finishes, and introduce out-of-roundness bore geometry.
2.2 Stacked Tolerance Accumulation
When a workpiece moves through multiple operations—for example, rough turning on a VTL, transfer to a floor-type boring mill for face milling, and a third step on a vertical center for bolt-circle drilling—each clamping cycle introduces fixture datum errors. Datum stacking routinely consumes up to 60% of total allowable drawing tolerances, leaving virtually zero margin for cutting tool wear or thermal expansion drift.
2.3 Complex Internal Geometries and Deep Recessing
Heavy hydraulic fluid ends, differential housings, and planet carrier sub-assemblies frequently feature complex internal profiles, including internal sealing grooves, taper seats, spherical radius bores, and back-facing shoulders. On standard HMCs lacking a dynamic contouring head, machining these features requires expensive, single-purpose right-angle heads or complex custom tooling that lacks rigidity and limits material removal rates.
3. Advanced Engineering Solutions: U-Axis Facing & Dual-Spindle Technology
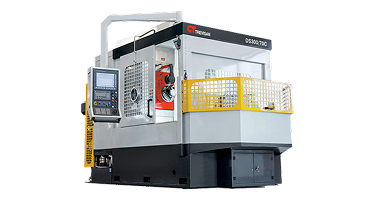
To overcome the physics limitations of turning heavy, asymmetrical parts, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. pioneered high-performance horizontal U-axis machining centers engineered specifically for heavy industrial components.
3.1 Kinematics of Stationary Part Machining
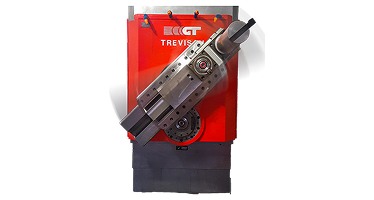
The core architectural principle of Nanjing Fortis Ag and construction CNC machinery is stationary part machining. Instead of spinning a massive, unbalanced 2,000 kg casting, the workpiece remains rigidly clamped to a high-capacity rotary index table or pallet system. The machine tool's integrated contouring facing head rotates the tool slide while dynamically adjusting the tool's radial position (U-axis) under full numerical control.
By rotating only the low-mass tool slide assembly rather than the heavy casting, centrifugal imbalance forces are practically eliminated. This allows high cutting speeds without vibration, yielding superior surface finishes (Ra 0.8 μm) and maintaining roundness tolerances within 0.008 mm even on 1,200 mm diameter bores.
3.2 Dual-Spindle Headstock Innovation
Nanjing Fortis horizontal machining centers feature an innovative dual-spindle configuration housed within a single heavy-duty headstock casing:
- Main Milling Quill Spindle: An oversized, heavy-duty gear-driven spindle quill designed for heavy face milling, deep hole drilling, tapping, and high-metal-removal roughing operations.
- Independent U-Axis Facing Head Spindle: A dedicated spindle equipped with an integrated sliding cross-feed mechanism. Controlled as a fully interpolated CNC U-axis, it executes outer diameter turning, inner diameter boring, facing, taper turning, thread chasing, and complex circular contouring using standard single-point carbide inserts.
This dual-spindle architecture provides seamless transition between heavy milling and precision turning operations without tool-head drop-off or manual head changing, drastically shortening total cycle time.
4. Comparative Engineering Analysis
To quantify the competitive advantage of modern Ag and construction CNC machinery against traditional manufacturing setups, the following matrix compares key operational parameters across standard industry configurations:
| Performance Metric | Traditional Line (VTL + HMC + Drilling Rig) | Standard 5-Axis HMC (Without Facing Head) | Nanjing Fortis Integrated U-Axis CNC System |
|---|---|---|---|
| Setup Clamping Cycles | 3 to 5 separate setups | 2 setups (requires special line-boring tooling) | 1 Single Setup (Fully Integrated) |
| Workpiece Kinematics | Part rotates at high RPM on VTL | Part stationary; limited to rotary milling | Part stationary; Tool rotates & contours (U-axis) |
| Concentricity / True Position | 0.035 mm - 0.060 mm (stack-up errors) | 0.020 mm - 0.030 mm | ≤ 0.008 mm (Single-datum machining) |
| Contouring & Thread Chasing | Requires standalone lathe arrangement | Limited; requires mechanical feed heads | Full CNC interpolation (U-axis tool slide) |
| Setup & Changeover Time | 4.5 - 6.0 Hours per batch | 2.0 - 3.5 Hours | < 45 Minutes (Automated pallet interchange) |
| Direct Operator Count | 3 Operators across cells | 1 to 2 Operators | 1 Operator (or Unattended Automation) |
5. Deep-Dive Component Applications in Agricultural & Construction OEMs
Applying specialized Ag and construction CNC machinery directly targets high-cost, bottleneck components found in heavy equipment production lines. Below are four technical case studies demonstrating real-world machining solutions.
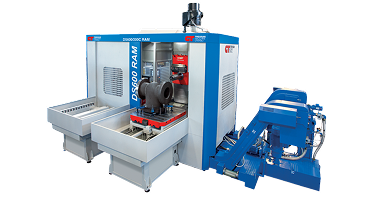
5.1 Heavy-Duty Tractor & Loader Axle Housings
Rigid planetary drive axle housings for high-horsepower agricultural tractors and wheel loaders require precise alignment between central differential mounting faces and outer planetary wheel hubs. Using traditional machinery, turning outer flange faces and boring internal bearing journals requires chucking the 3-meter housing on a VTL, leading to severe deflection at the unsupported extended end.
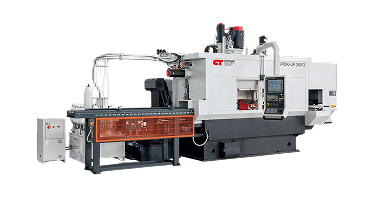
With Nanjing Fortis horizontal U-axis machinery, the axle housing is clamped motionless on a dual-pallet shuttle system. The integrated U-axis facing head mills flange faces, bores multi-stage bearing pockets, cuts internal retaining ring grooves, and single-point chases thread profiles up to 600 mm diameter in one continuous sequence. concentricity between left and right axle bores is held within 0.010 mm across a 2,500 mm span.
5.2 High-Pressure Hydraulic Valve Manifolds & Pump Bodies
Hydraulic excavators and mobile cranes operate under extreme fluid pressures exceeding 350 bar. Their main hydraulic control blocks and variable-displacement pump bodies require flawless internal valve bores, deep internal seal cavities, and O-ring grooves. Any tool chatter marks or out-of-roundness leads to fluid bypass and hydraulic power drop.
Utilizing the high-rigidity spindle quill combined with U-axis internal contouring, Nanjing Fortis machines complete precision boring, back-spotfacing of internal ports, and mirror-finish burnishing on cast ductile iron pump housings without removing the part from the fixture. Scrap rates caused by internal seal leakage are virtually reduced to zero.
5.3 Track Frames, Excavator Swivel Joints & Boom Arms
Excavator track roller frames and boom swivel joints are subject to immense torsional forces. Machining these weldments involves heavy face milling across interrupted cuts on flame-cut steel plates. Nanjing Fortis heavy-duty box-way machining centers feature high-torque gearheads delivering up to 3,200 Nm of spindle torque at low speeds, enabling deep-depth-of-cut roughing (up to 8 mm per pass) while maintaining thermal stability over long cutting cycles.
5.4 Specialized and Custom OEM Machinery Needs
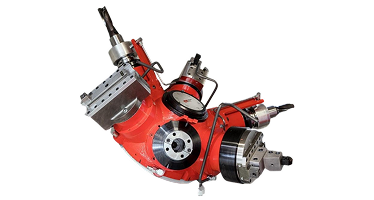
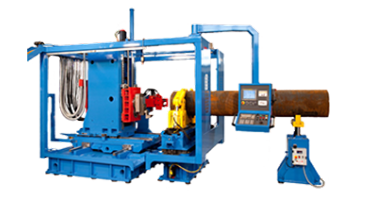
When standard catalog machine configurations cannot fulfill unique factory floor layouts or non-standard component envelopes, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. leverages over six decades of custom machine tool engineering experience. From multi-spindle transfer lines to customized bed-length horizontal U-axis platforms, customized machinery integrates seamlessly with automated guided vehicles (AGVs) and robotic cell loaders.
6. Total Cost of Ownership (TCO) & Financial ROI Model
Procurement directors and capital expenditure (CapEx) committees evaluating Ag and construction CNC machinery must weigh initial equipment acquisition costs against long-term operational expenditure (OpEx) benefits. Single-setup U-axis machining technology transforms financial payback metrics across four core operational areas:
6.1 Direct Labor Reduction
Consolidating three standalone machines (VTL + HMC + Radial Drill) into one Nanjing Fortis U-axis machining center eliminates two operator shifts. In typical North American and European manufacturing environments, saving two skilled machinist positions yields $160,000 to $220,000 in annual direct labor savings per machine cell.
6.2 Cycle Time and TAKT Time Compression
Eliminating inter-machine part queueing, overhead crane lifting, manual datum re-alignment, and multiple clamping verification steps cuts total throughput time per part by 40% to 65%. A planetary axle housing requiring 4.5 hours of total handling and cutting time across a traditional cell is completed in under 75 minutes on an integrated Nanjing Fortis horizontal U-axis machining center.
6.3 Floor Space and Facility Footprint Efficiency
A single integrated machining center occupies up to 50% less floor area than a multi-machine cell with interim part staging buffers. Facility cost allocations per square meter are drastically lowered, freeing up high-bay manufacturing space for final assembly lines.
6.4 Tooling Expense Optimization
Because the CNC U-axis facing head uses standard off-the-shelf single-point turning inserts to profile a wide range of bore diameters and chamfers, factory inventory of large, expensive, custom-ground boring bars is cut dramatically. Tooling procurement expenses drop by an average of 30% annually.