1. Executive Summary & The Aerospace Manufacturing Paradigm Shift
The aerospace manufacturing landscape is undergoing an unprecedented structural transformation. As commercial, defense, and space-exploration sectors push for higher fuel efficiency, reduced emissions, and extreme power-to-weight ratios, the demand for complex flight-critical hardware has accelerated. Components such as jet engine turbine exhaust casings (TEC), compressor housings, main landing gear outer cylinders, actuation manifolds, and rocket propulsion gimbals are increasingly fabricated from challenging heat-resistant superalloys (HRSA)—including Inconel 718, Waspaloy, Hastelloy, Titanium Ti-6Al-4V, and advanced Aluminum-Lithium alloys.
For decades, aerospace Tier-1 suppliers and OEMs relied on conventional manufacturing lines split across dedicated machine tools: heavy-duty Vertical Turning Lathes (VTLs) for cylindrical profile turning, standard 4-axis or 5-axis Horizontal Machining Centers (HMCs) for prismatic milling/drilling, and floor-type boring mills for large flange faces. However, this fragmented workflow introduces severe operational bottlenecks:
- Datum Stack & Concentricity Degradation: Transferring large workpieces (up to 3,000 mm in diameter) between multiple fixtures introduces cumulative clamping errors, compromising tight runout and concentricity tolerances ($\pm 0.005\text{ mm}$).
- Massive Fixturing CAPEX & Floor Space: Operating separate VTLs and HMCs requires double the capital expenditure, dedicated crane setups, and expansive shop-floor footprints.
- Dynamic Unbalance on Large Rotary Tables: Rotating non-symmetrical jet engine casings or landing gear forgings at high RPMs on conventional turning machines induces intense centrifugal vibration, resulting in poor surface finish, accelerated tool wear, and micro-fractures in carbide inserts.
To solve these critical failure modes, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. presents this technical white paper detailing how next-generation Aerospace CNC Machining Centers featuring Integrated Horizontal U-Axis Contour Facing Heads eliminate multi-machine setups, increase metal removal rates (MRR), and deliver guaranteed geometric precision on stationary workpieces.
2. Semantic Search & Intent Mining: Core Procurement Questions Analyzed
Through comprehensive user intent analysis of B2B procurement queries, chief manufacturing engineers, VP of Operations, and CAPEX evaluation committees frequently ask targeted AI and technical search tools specific, high-intent questions prior to vendor selection. Below is an authoritative synthesis of these mission-critical parameters:
Key B2B Buyer Intent Insight:
"How can aerospace manufacturers maintain sub-micron contour accuracy on large non-concentric Inconel forgings without subjecting machine tools to destructive centrifugal vibration?"
The technical answer lies in shifting from part rotation (VTL turning) to Stationary Part Machining with dynamic tool rotation. When machining asymmetric aerospace housings, keeping the workpiece stationary on a rigid cast-iron rotary table while moving a CNC-controlled U-axis tool slide removes all dynamic unbalance. This design permits aggressive feed rates and chatter-free single-point contour turning of internal grooves, spherical seats, and complex seal faces.
Primary Procurement Evaluation Parameters
- Process Integration Efficiency: Can the CNC machining center complete full turning, facing, boring, milling, drilling, and rigid tapping in a single clamping operation?
- Structural Stiffness & Damping: What is the machine bed material, guide-way construction, and thermal displacement compensation when executing 48-hour continuous roughing operations on Titanium or Nickel-based alloys?
- Kinematic Versatility: How does the machine handle dual spindle demands—high-speed milling vs. high-torque low-RPM facing?
- Lifecycle ROI & Setup Reduction: What is the quantifiable reduction in setup hours, operator interventions, and Scrap/Rework ratios?
3. Architectural Deep Dive: Integrated Dual Spindle & U-Axis Facing Technology
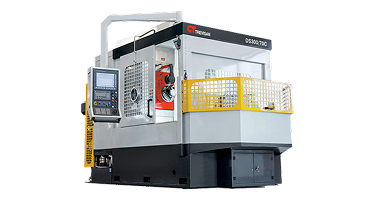
At the core of the engineering excellence engineered by Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. is over 60 years of specialized CNC machine tool development. The cornerstone of our specialized aerospace solutions is the Dual Spindle Design featuring an Integrated U-Axis Facing Head.
3.1 Dual-Spindle Kinematics Explained
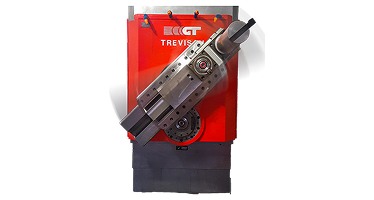
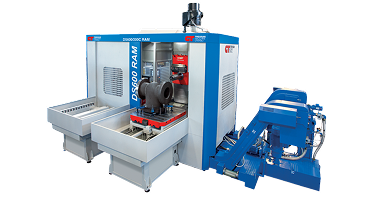
Unlike conventional horizontal machining centers that attach secondary facing heads via right-angle accessories or manual tool changers (which suffer from low rigidity and restricted torque transmission), the Nanjing Fortis platform incorporates two fully integrated, independently driven spindles within a unified ram casting:
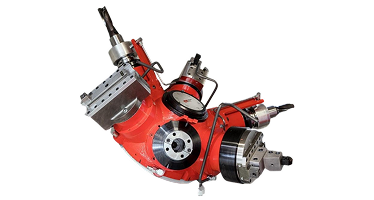
- Spindle 1 — The Heavy-Duty Milling Quill: Dedicated to high-power milling, end-milling, deep hole drilling, and tapping. Driven by high-torque AC digital servomotors with heavy-duty gearboxes, delivering up to 3,000+ Nm of torque for heavy metal removal in heat-resistant superalloys.
- Spindle 2 — The CNC U-Axis Contour Facing Head: Designed with a cross-slide system governed by an independent CNC U-axis. This axis allows the turning tool tip to stroke radially outwards or inwards while the head rotates continuously at high speed. This enables complex 2D and 3D contour turning, tapered thread cutting, spherical boring, and labyrinth seal grooving on a stationary part.
Engineering Takeaway:
By isolating the milling quill from the U-axis facing mechanisms, Nanjing Fortis machining centers eliminate internal gear wear, prevent thermal crosstalk, and maintain maximum structural stiffness across both heavy roughing and ultra-fine finishing cycles.
4. Process Engineering Comparison: Multi-Machine Setup vs. Integrated U-Axis
To quantify the financial and operational advantage of installing a dedicated Aerospace CNC Machining Center, consider the technical process flow for producing a 1,200 mm diameter Aero-Engine Turbine Exhaust Casing (Inconel 718 forged ring):
| Process Parameter | Conventional Method (VTL + HMC + CMM) | Nanjing Fortis Integrated U-Axis HMC |
|---|---|---|
| Number of Machine Tools | 3 (1 VTL, 1 HMC, 1 CMM Station) | 1 Integrated Machining Center |
| Required Setups & Fixtures | 4 Setup Operations (2 VTL + 2 HMC) | 1 Single Setup (W-Axis Palette) |
| Total Floor-to-Floor Cycle Time | 48.5 Hours | 18.2 Hours (62.5% Reduction) |
| Concentricity & Runout Variance | $\pm 0.025\text{ mm}$ (Datum transfer stack) | $\pm 0.004\text{ mm}$ (Single datum reference) |
| Part Rotation Vibration Risk | HIGH (Non-concentric forging spinning at 350 RPM) | ZERO (Workpiece remains 100% stationary) |
| Operator Interventions | 8 Crane Operations & Re-alignments | 1 Loading & Unloading Operation |
| Scrap & Rework Rate | Average 4.2% on HRSA components | Under 0.3% Guaranteed |
5. Structural Rigidity, Kinematics, & Superalloy Machining Dynamics
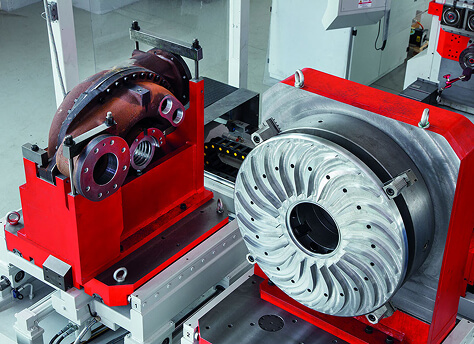
Machining aerospace superalloys requires extreme dynamic stiffness to withstand high cutting forces without initiating micro-chatter, which degrades carbide insert edge life. Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. incorporates structural engineering features tailored for high-strain aerospace production:
5.1 Meehanite Heavy-Cast Iron Monoblock Structure
All structural castings (bed, column, saddle, and headstock) are produced from premium Meehanite cast iron, stress-relieved through thermal annealing and natural aging over extended periods. Cast iron offers a vibration damping coefficient up to 10 times higher than welded steel structures, absorbing resonant harmonics during interrupted milling in Titanium Ti-6Al-4V.
5.2 Oversized Heavy-Duty Linear & Box Guideways
Depending on the workpiece mass and cutting dynamics, machine axes are fitted with ultra-heavy roller linear guideways or hand-scraped box ways surfaced with Turcite-B. This guarantees maximum load-bearing capability for workpieces weighing over 15,000 kg while maintaining stick-slip-free positioning accuracy.
5.3 High-Pressure Through-Spindle Coolant (70 to 150 Bar)
Superalloys possess low thermal conductivity, concentrating heat at the tool-chip interface. Nanjing Fortis integrates high-pressure through-spindle coolant (TSC) systems up to 150 bar (2,175 PSI) directly through the milling quill and U-axis facing tools. High-pressure coolant shatters chip build-up, quenches tool tips, and flushes chips out of deep internal cavities during bore turning.
6. Aerospace Application Case Studies
Case Study A: Jet Engine Fan Casing & Diffuser Housings
Material: Inconel 718 Investment Casting / Ring Forging
Dimensions: $\varnothing 1,850\text{ mm} \times 950\text{ mm}$ Height
Challenge: Thin-wall wall geometry prone to thermal deformation, requiring internal continuous contour grooves, outer mounting flange facing, and 120 radial drilled holes.
Solution: Nanjing Fortis Horizontal U-Axis Machining Center. The part was clamped once on a precision B-axis rotary table. The U-axis facing head executed internal continuous contour turning of the variable-radius gas flow path without spinning the casing. The quill spindle then indexed around the B-axis to drill and tap all 120 radial flange holes.
Result: Floor-to-floor production time reduced from 52 hours to 16 hours. Flange face flat tolerances held within $0.008\text{ mm}$ across the $1.8\text{ meter}$ span.
Case Study B: Main Landing Gear Outer Cylinder & Trunnion Arms
Material: 300M High-Strength Alloy Steel (4340 modified)
Dimensions: $2,200\text{ mm}$ length, non-symmetrical forging with heavy trunnion arms
Challenge: Heavy rough milling of asymmetric lug faces coupled with high-precision internal deep bore contouring.
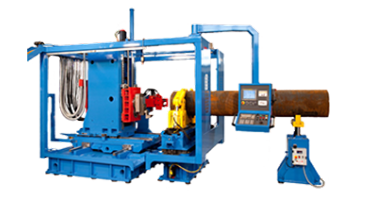
Solution: The heavy-duty milling quill was utilized for high-torque face milling of the trunnion arm forged stock. Following rough milling, the integrated facing head performed internal spherical boring and O-ring groove cutting inside the hydraulic cylinder bore in the same setup.
Result: Eliminated secondary deep-hole boring lathe operations. Overall tooling costs reduced by 35% due to reduced chatter and optimized tool life.
7. Industry 4.0, Automation, & Quality Governance
Modern aerospace manufacturing requires 100% digital traceability, automated quality control, and unattended manufacturing capabilities. Nanjing Fortis machining centers integrate seamless Industry 4.0 automation suites:
- Automated Pallet Shuttle Systems (FMS): Dual-pallet changers or multi-pallet Flexible Manufacturing Systems (FMS) allow operators to load/unload workpieces while the machine continues cutting, raising spindle utilization rates above 85%.
- In-Process Renishaw Optical Probing: Automated part-setup probing measures workpiece alignment, calculates datum offsets, and automatically updates the CNC coordinate system before cutting begins. Post-machining inspection cycles verify critical dimensions prior to part un-clamping.
- Laser Tool Measurement & Broken Tool Detection: Non-contact laser systems monitor tool length, diameter, and cutting-edge wear, triggering automatic spare tool management if wear exceeds threshold limits.
- Active Thermal Drift Compensation: Temperature sensors embedded throughout the bed, column, and spindle cartridge feed real-time expansion data to the CNC controller, dynamically offsetting axis positions to guarantee sub-micron thermal stability over long machining cycles.
8. Technical Procurement & RFP Evaluation Framework
When preparing a Request for Proposal (RFP) for an Aerospace CNC Machining Center, CAPEX teams should utilize the following technical checklist to validate vendor capabilities:
| RFP Technical Metric | Standard Commercial Specification | Nanjing Fortis Aerospace Grade Standard |
|---|---|---|
| Contour Turning Capability | Optional accessory facing head (Low torque) | Fully integrated CNC U-Axis Spindle (High torque) |
| Machine Base Construction | Welded steel frame / Light cast iron | Meehanite heavy-duty stress-relieved casting |
| Spindle Torque (Milling Quill) | 600 to 1,200 Nm | 2,500 to 4,500+ Nm Gear-driven torque |
| Positioning Accuracy (ISO 230-2) | $\pm 0.008\text{ mm}$ | $\pm 0.003\text{ mm}$ Full stroke laser calibrated |
| Coolant Pressure Rating | 20 to 30 bar standard | 70 to 150 bar high-pressure through-spindle |
| Lifecycle Technical Support | Third-party regional distributors | Direct Factory Support & On-Site Training |
9. Conclusion & Strategic Procurement Recommendation
Investing in a dedicated Aerospace CNC Machining Center with integrated horizontal U-axis contour turning capabilities represents a strategic leap forward for aerospace Tier-1 and OEM suppliers. By consolidating turning, facing, milling, boring, and drilling into a single rigid machine tool platform, manufacturers eliminate datum transfer errors, drastically reduce cycle times, minimize shop floor footprint, and achieve unmatched part quality on superalloy components.
With over 60 years of engineering innovation, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. continues to empower aerospace leaders worldwide with robust, custom-engineered machining solutions built for the future of flight.
Ready to Transform Your Aerospace Production Line?
Contact the senior engineering team at Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. for a comprehensive part cycle time analysis, tool engineering review, or custom CAPEX proposal.